


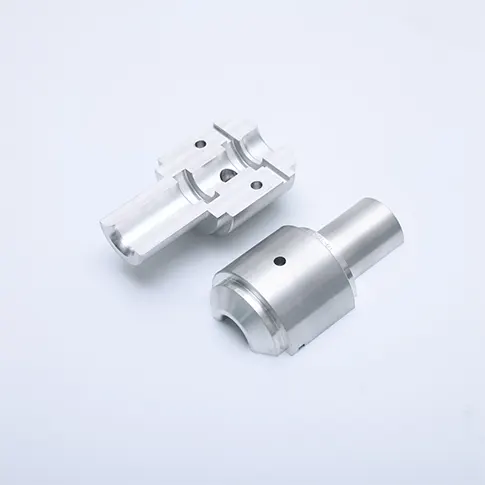
5-Axis CNC Machining for Deep Cavities | Design & Tool Access
Deep cavities are common in precision housings, aerospace components, industrial equipment, automotive parts, and custom metal components. However, machining these features can be difficult because the cutting tool must reach deep into the workpiece while maintaining sufficient rigidity, avoiding collisions, and removing chips effectively.
5-axis cnc machining for deep cavities can improve access to angled walls, complex internal features, and multi-sided geometries. By adjusting the tool orientation, manufacturers may be able to use more suitable cutting approaches and reduce the number of setups. The results still depend on cavity geometry, tool length, machine configuration, material, and machining strategy.
For engineers and B2B buyers, understanding deep-cavity design and tool access helps improve manufacturability, manage machining costs, and select a supplier capable of producing complex CNC machined parts.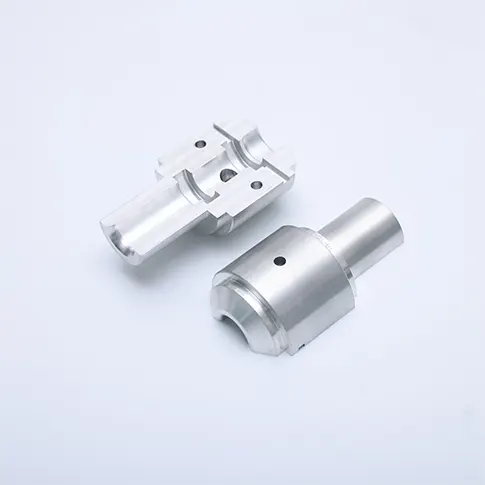
1. Why Are Deep Cavities Difficult to Machine?
As cavity depth increases relative to its width, tool access becomes more restricted. The cutting tool and holder must reach the required surfaces without contacting the surrounding walls, while the tool must remain rigid enough to remove material consistently.
Common challenges in deep cavity CNC machining include:
Limited tool access: Narrow openings and deep walls may restrict the tool diameter, holder size, and available approach angles.
Tool deflection: Long-reach tools can bend under cutting forces, affecting dimensional accuracy and surface finish.
Chatter and vibration: Reduced tool rigidity can increase vibration, noise, tool wear, and the risk of poor surface quality.
Chip evacuation: Chips can accumulate inside a cavity, interfering with cutting and potentially damaging the tool or workpiece.
Heat management: Restricted access can make coolant delivery and heat removal more difficult.
Collision risk: The tool holder, spindle, fixture, or machine structure may interfere with the workpiece during complex movements.
These problems are closely related. For example, a narrow cavity may require a smaller-diameter, longer tool, which reduces rigidity and can increase vibration. Effective planning must therefore consider the entire tool assembly rather than the cutter alone.
2. How Does 5-axis CNC machining Improve Tool Access?
A five-axis CNC machine combines three linear axes with two rotary axes. Depending on the machine design, the additional rotary movement changes the orientation of the cutting tool, the workpiece, or both.
For complex cavities, 5-axis CNC milling may offer several advantages:
Angled tool approach: The tool can approach certain inclined walls or features from a more suitable direction.
Reduced repositioning: Multiple cavity surfaces may be accessible in one setup, depending on the geometry and machine envelope.
Improved holder clearance: Tilting the tool may provide additional clearance between the holder and surrounding walls.
Flexible toolpath planning: Tool orientation can be adjusted to suit different surfaces and cutting conditions.
Complex geometry support: Compound-angle surfaces and certain internal features may be easier to access than with a fixed tool orientation.
However, five-axis machining does not eliminate the physical limitations of tool reach or stiffness. A cavity with a very narrow opening may still require a long-reach tool, specialized tooling, alternative machining operations, or a design change. Some deep cavities can also be produced efficiently on three-axis or four-axis equipment.
3. Design Cavity Depth, Width, and Corner Radii for Manufacturability
Part geometry has a direct effect on tool selection and machining time. Before releasing a design for production, engineers should consider the relationship between cavity depth, opening width, wall angle, and internal corner geometry.
Cavity Depth-to-Width Ratio
Deeper and narrower cavities generally require longer-reach tools and create greater access challenges. When the design allows, increasing the cavity opening or reducing unnecessary depth can make machining easier. There is no universal depth-to-width limit because the practical range depends on the tool diameter, material, tool construction, and required accuracy.
Internal Corner Radius
A milling cutter cannot produce a perfectly sharp internal corner. The resulting radius depends on the cutter geometry and toolpath. Very small internal radii may require smaller tools, additional machining passes, or alternative processes, potentially increasing cycle time.
Where sharp corners are not functionally necessary, specifying a suitable internal radius can improve tool rigidity and reduce manufacturing cost.
Opening Width and Holder Clearance
The cavity opening must accommodate the cutting tool and, where relevant, the tool holder. Even if the cutter diameter fits, the larger holder may collide with the cavity walls at certain tool angles. Checking the complete tool assembly in the CAD/CAM environment helps identify these limitations before machining begins.
Wall Angles and Undercuts
Angled walls and undercuts can limit access from a vertical direction. Five-axis positioning may provide access to some of these features, but the achievable geometry depends on rotary travel, tool length, holder shape, and machine kinematics. Features that cannot be reached safely may require a different design or additional manufacturing process.
4. Choose the Right Cutting Tool for Deep Cavities
Tool selection is a major factor in the quality and efficiency of deep cavity CNC milling. The objective is to reach the required surfaces while maintaining sufficient rigidity and effective chip evacuation.
Tool Diameter and Reach
A larger-diameter tool is generally more rigid than a smaller tool of comparable construction, but it may not fit into narrow cavities or small internal radii. The tool diameter and overhang should therefore be selected together with the cavity geometry.
Tool Material and Geometry
Tool material, flute design, cutting-edge geometry, coating, and overall tool construction should match the workpiece material and cutting operation. Suitable tooling can help control wear and improve cutting stability, but the best choice depends on the specific application.
Long-Reach and Extended-Reach Tools
Long-reach tools provide access to deep features but are more sensitive to deflection and vibration. The required reach should be minimized where possible, and tool overhang should not be greater than necessary. For demanding applications, the supplier may need to evaluate tool rigidity and cutting conditions through CAM simulation or trial machining.
5. Optimize Tool Orientation and Toolpath Strategy
Five-axis machining allows tool orientation to change throughout the toolpath or between machining operations. The correct strategy depends on the cavity's shape, the required surface quality, and the available machine configuration.
Plan Toolpaths Around the Cavity Geometry
Roughing, semi-finishing, and finishing may be planned as separate operations. Roughing removes the majority of the material, while semi-finishing helps establish a more consistent allowance for the final pass. Finishing then focuses on achieving the specified dimensions and surface condition.
Maintain Suitable Tool Engagement
Tool engagement affects cutting forces, heat generation, and vibration. Appropriate radial engagement, axial depth, feed rate, and spindle speed should be selected according to the material and tooling. A toolpath that maintains stable engagement may reduce sudden load changes and improve machining consistency.
Use Tool Tilting Where It Provides a Benefit
Tilting the tool can improve access or create clearance in some cavities. However, unnecessary changes in tool orientation may increase programming complexity or introduce additional kinematic challenges. The selected orientation should provide a clear manufacturing benefit and remain within the machine's safe operating envelope.
Simulate the Complete Tool Assembly
CAM simulation should consider the cutter, holder, spindle, workpiece, and fixture where the software and machine model allow. Collision checks and axis-travel verification are particularly important for deep cavities and complex five-axis movements. Simulation reduces programming risk but does not replace machine setup checks and appropriate process validation.
6. Manage Chip Evacuation and Heat
Chip removal is particularly important when machining deep or narrow cavities. If chips remain trapped in the cutting zone, they may be recut, increase tool wear, damage the surface, or interrupt the process.
Depending on the material and machine configuration, manufacturers may consider:
Suitable coolant delivery to the cutting zone
Tooling designed for the material and cavity geometry
Toolpaths that provide space for chips to escape
Appropriate cutting parameters to control chip formation
Intermediate chip-clearing operations where required
Monitoring of tool wear, cutting load, and surface condition
Coolant delivery and chip evacuation should be considered during process planning rather than treated as final adjustments. The appropriate approach varies by material, cavity dimensions, tool type, and machine capabilities.
7. Control Dimensional Accuracy and Surface Finish
Deep cavities can be difficult to inspect because measuring equipment may have limited access to internal walls and bottom surfaces. In addition, tool deflection and vibration may cause the actual cavity geometry to differ from the programmed dimensions.
Buyers and engineers should define inspection requirements clearly, including:
Cavity dimensions: Specify depth, width, length, and relevant dimensional tolerances.
Internal corner radii: Identify required radii and any features that must remain accessible to the selected inspection method.
Wall profile and angle: Define geometric requirements for inclined surfaces and complex profiles.
Surface roughness: Specify the required finish for functional surfaces rather than applying unnecessarily strict requirements to every surface.
Datum references: Establish the datum structure needed to verify cavity location and alignment.
Inspection access: Confirm that the specified features can be measured using the proposed equipment and inspection setup.
Depending on the part geometry and tolerances, inspection may involve coordinate measuring machines, suitable probes, optical systems, or other appropriate methods. The measurement approach should be agreed upon before production when internal features are difficult to access.
8. What Affects the Cost of 5-Axis CNC Machining for Deep Cavities?
The cost of deep-cavity machining depends on more than the number of machine axes. Geometry, tool requirements, programming time, cycle time, workholding, and inspection all influence the final quotation.
Cavity depth and opening width: Deep, narrow features may require specialized tools and more conservative cutting conditions.
Corner radii: Very small radii can require smaller cutters and additional machining passes.
Material: Difficult-to-machine alloys may require different tools, cutting parameters, and longer production time.
Geometric complexity: Compound angles and restricted tool access may increase CAM programming and verification effort.
Tolerances and surface finish: Tight requirements can increase finishing and inspection time.
Production quantity: Prototype and small-batch orders may have different setup-cost distribution from repeat production.
To control costs, buyers can review cavity geometry with the manufacturer before finalizing the design. Increasing a non-critical corner radius, improving tool access, or relaxing an unnecessary tolerance may reduce machining complexity without affecting the component's intended function.
9. How to Evaluate a Deep-Cavity CNC Machining Supplier
When sourcing custom 5-axis CNC machined parts, buyers should assess the supplier's experience with similar geometries, tooling strategy, programming capability, and inspection process.
Useful questions include:
Has the supplier machined similar cavity depths, opening widths, materials, and internal radii?
Can the supplier review 3D models and identify tool-access or holder-clearance problems?
Does the supplier use CAM simulation and collision checking for complex five-axis operations?
How will cavity dimensions, wall angles, and surface finish be inspected?
Can the supplier provide inspection reports or material documentation where required?
What are the expected prototype lead time, production lead time, and batch capacity?
Providing a complete drawing package helps the supplier evaluate the project more accurately. Include the 3D CAD model, 2D drawing, material grade, critical tolerances, surface finish requirements, order quantity, and any special inspection requirements.
Frequently Asked Questions
Is 5-axis CNC machining always necessary for deep cavities?
No. Some deep cavities can be machined efficiently using three-axis or four-axis equipment. Five-axis machining is particularly useful when tool orientation, angled surfaces, restricted access, or multiple setups create a clear manufacturing advantage.
How does cavity depth affect CNC machining accuracy?
Greater cavity depth can require longer tools, which are more susceptible to deflection and vibration. Restricted access may also complicate chip evacuation and inspection. Tool selection, cutting strategy, fixture design, and process validation help manage these challenges.
How can I reduce the cost of deep-cavity CNC machining?
Review cavity depth, opening width, internal corner radii, material choice, tolerances, and surface finish requirements. Improving tool access and avoiding unnecessarily tight specifications can reduce tool complexity, machining time, and inspection costs.
Can five-axis machining produce internal undercuts?
Some undercuts and angled internal features can be machined using suitable five-axis tool orientations and tooling. Feasibility depends on the opening size, feature geometry, holder clearance, machine travel, and available cutting tools. Certain geometries may require alternative processes.
What information should I provide for a deep-cavity CNC machining quote?
Provide a 3D CAD model, 2D drawing, material specification, cavity dimensions, critical tolerances, surface finish requirements, quantity, and delivery expectations. Marking critical internal features helps the supplier assess tooling, accessibility, and inspection requirements.
Request a Quote for 5-Axis CNC Machining
Deep-cavity components require careful coordination between part design, tool selection, CAM programming, chip evacuation, and inspection. Reviewing tool access and manufacturability early can help reduce machining risks and improve production efficiency.
Send your CAD model, engineering drawing, material requirements, and target quantity to discuss your deep-cavity CNC machining project.